Global buyers entering 2026 face a crowded market for Belt Conveying Equipment. Catalogues look impressive. Real performance is less obvious.
David J. Alspaugh, a recognized conveyor weighing specialist, has emphasized this practical principle: “Reliable material handling depends on accurate measurement, controlled movement, and disciplined maintenance.” His view remains relevant for mining, aggregates, ports, cement plants, recycling facilities, and warehouse operations. Equipment must match the material, route, climate, duty cycle, and local service capacity. A belt conveyor carrying wet limestone needs different protection from one moving dry grain. Small details matter. Belt width, pulley diameter, idler spacing, skirting, dust control, and emergency stops can influence the entire project.
This guide examines the leading Belt Conveying Equipment options expected to attract global buyers in 2026. It considers conveyor capacity, energy consumption, intelligent monitoring, modular design, installation access, spare-part availability, and supplier expertise. Field experience often reveals more than a polished brochure. A transfer chute may appear efficient, yet create hidden spillage. A low-cost belt may seem attractive, yet fail under abrasive loading. These risks deserve careful review.
No buying guide is flawless. Site conditions change. Supplier data can also be incomplete. Buyers should verify test results, certifications, warranty terms, maintenance records, and references from comparable installations. The strongest choice is not always the newest system. It is the equipment that delivers safe, stable, measurable performance over years of operation. Reliability takes patience. Mistakes become expensive.
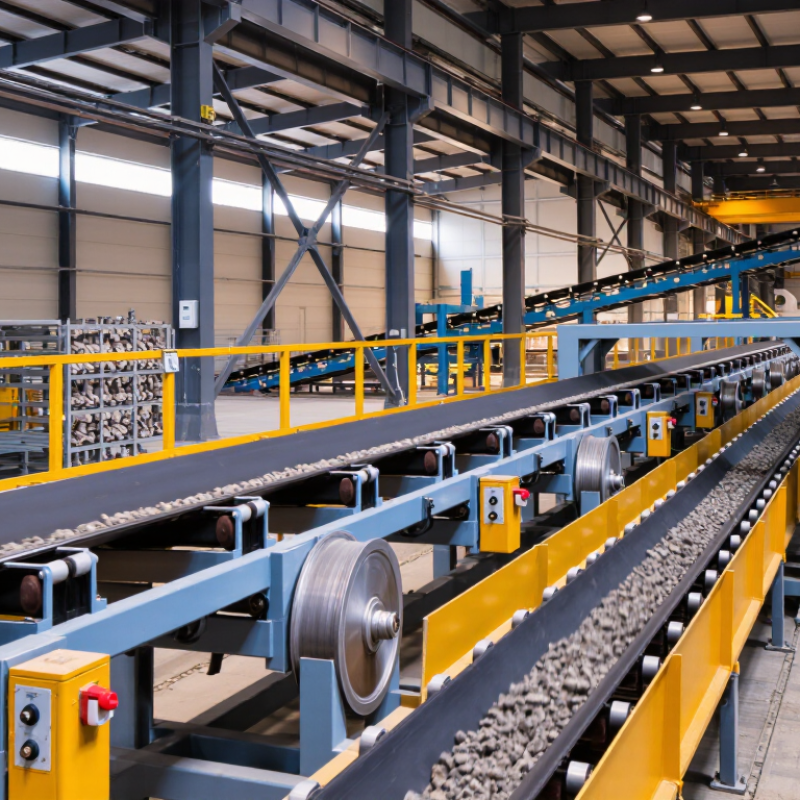
Belt conveying equipment moves bulk materials or packaged goods on a continuous belt. A motor drives a pulley, while rollers support the belt and its load. The belt travels between the tail and discharge ends. Materials enter through a loading chute and leave at the selected discharge point. Simple in principle. Careful design matters.
In practical installations, engineers match belt width, speed, tension, and frame strength to the material. Heavy stone needs stronger components than sealed cartons. Dust, moisture, heat, and sharp edges also affect belt selection. A tracking system keeps the belt centered during operation. Scrapers remove carryback near the discharge pulley. Emergency stops, guards, and accessible inspection points improve workplace safety. Misalignment is often blamed on the belt, but uneven loading may be the real cause. That detail is easy to miss.
Tips: Confirm the material’s weight, size, temperature, and moisture before choosing equipment. Leave safe access around service areas. Check pulley alignment and belt tension regularly. Listen for unusual noise. Small changes can signal worn bearings or slipping belts. Buyers should request load calculations, maintenance guidance, test records, and clear safety documentation. A low purchase price may become expensive when cleaning, downtime, and replacement parts are ignored. Performance also depends on installation quality, not only equipment specifications.
Belt conveying equipment transports bulk materials or packaged goods on a continuous moving belt. A motor-driven pulley powers the belt, while idlers support the load and a take-up system maintains proper tension.
Indicative throughput by belt width: The chart uses common engineering reference values for bulk material conveying at a belt speed of 2.0 m/s and a bulk density of 1.6 t/m³. Actual capacity depends on belt trough angle, material characteristics, loading conditions, incline, and safety factors.
Belt conveyors vary by product shape, distance, and working environment. Flat belt conveyors suit warehouses, packaging lines, and light material handling. They provide a stable surface for cartons and individual products. Troughed belt conveyors carry bulk materials such as coal, gravel, grain, and crushed stone. Their angled rollers help reduce spillage during transport.
Cleated belt conveyors are useful for inclined movement. Cleats keep bags, boxes, and loose materials from sliding backward. In food processing, hygienic flat conveyors often use easy-clean surfaces and corrosion-resistant frames. Pipe belt conveyors can protect dusty materials from wind and moisture. Curved belt conveyors save floor space in distribution centers. Each design has limits. A conveyor selected only by capacity may still create noise, belt wear, or difficult cleaning.
Tips: Measure the material before choosing the belt. Record its weight, moisture, temperature, and particle size. Check the required speed and elevation. Leave access around pulleys and emergency stops. Ask for load testing when the application is unusual. I have seen projects fail because return-belt cleaning was ignored. Small details matter. A practical review should include maintenance skill, spare-part availability, local electrical standards, and installation conditions. Sometimes a slower conveyor performs better because it protects fragile goods and reduces belt tracking problems.
For global buyers, belt conveying equipment should be compared by operating conditions, not catalog appearance. A practical review begins with rated capacity, belt width, belt speed, and material density. A 1,000 mm belt can handle different tonnage at 0.8 m/s and 2.5 m/s. Check both average flow and peak loading. Peak loads matter. Incline, transfer height, and route length also affect motor sizing. Moisture, abrasiveness, temperature, and particle size can change the selection.
Frame construction, pulley diameter, idler spacing, and belt tension deserve close attention. A heavier frame may improve stability but increase installation costs. Motor power should match the duty cycle, starting method, and conveyor length.
Ask for load calculations, test records, noise data, and maintenance intervals. Clear documentation supports reliable purchasing decisions. It also helps engineers compare equipment fairly across different countries and operating standards.
Safety and service access are practical specifications, not optional details. Guarding, emergency-stop devices, belt misalignment detection, and accessible inspection points reduce operational risk. Dust control may require sealed transfer areas and suitable cleaning systems. A common mistake is choosing the lowest initial price. Field inspections often show that poor alignment, overloaded idlers, and difficult belt replacement create larger costs later.
I would not treat every published capacity as guaranteed performance. Actual results depend on installation quality, material behavior, and disciplined maintenance. Spare-part availability and technician training should be checked before purchase.
How Global Buyers Can Select the Right Conveyor System
Choosing belt conveying equipment starts with the material, not the catalog image. Measure bulk density, moisture, particle size, temperature, and expected throughput. A belt handling dry grain may fail quickly with sticky clay. Real site conditions matter.
Walk the route before comparing quotations. Record conveyor length, incline angle, transfer points, available power, dust levels, and ambient temperature. Belt width should match loading volume without creating unnecessary energy use. Ask for motor efficiency data, belt specifications, guarding details, emergency-stop locations, and test procedures. Local electrical requirements and safety standards also need confirmation. These details can prevent expensive redesigns.
Maintenance access deserves equal attention. Check whether workers can reach rollers, scrapers, sensors, and take-up units safely. Request a clear spare-parts list and realistic service intervals. I have seen projects focus on purchase price while ignoring belt tracking problems near transfer points. That choice looked efficient on paper, but downtime changed the calculation. A site trial or factory acceptance test can reveal vibration, spillage, and misalignment earlier. Still, no test can reproduce every season or operator habit. Leave adjustment space in the design. Good equipment should fit the operation, not force the operation to fit the equipment.
In 2026, belt conveyor sourcing is shifting from simple price comparison to lifecycle performance. Buyers increasingly examine energy use, maintenance access, safety controls, and spare-part availability. This reflects real operating pressure in warehouses, mines, ports, and processing plants. A conveyor may run thousands of hours yearly, often in dust, humidity, or temperature changes. Small details matter.
Energy-efficient motors, variable-speed drives, and improved belt tracking are becoming standard requirements. Condition-monitoring sensors can detect bearing heat, belt misalignment, and abnormal vibration before a shutdown occurs. Digital commissioning tools also help teams test layouts before installation. However, not every smart sensor delivers useful data. I have seen systems produce alerts that operators could not interpret. Simple dashboards often work better.
Global buyers should request verified load calculations, belt specifications, noise data, and maintenance procedures. They should also confirm electrical compatibility and local service capability before signing a contract. Factory inspections remain valuable, especially when checking weld quality, pulley balance, guarding, and emergency-stop response. A low-cost quotation can hide expensive installation changes. Delivery promises may also overlook customs clearance and replacement-part lead times. I still find that a detailed acceptance test prevents more disputes than impressive sales language.
| Equipment Category | Typical Belt Width | Typical Capacity | Typical Belt Speed | Suitable Incline Range | Common Applications | Key 2026 Technology Trend | Important Sourcing Criteria |
|---|---|---|---|---|---|---|---|
| Standard Troughed Belt Conveyor | 500–2,400 mm | 100–10,000 t/h | 0.8–5.0 m/s | Generally up to 15° for loose bulk materials | Aggregates, cement, mining, ports, power generation and bulk material handling | Higher-efficiency drives, enclosed transfer points, belt condition monitoring and energy-efficient idlers | Conveyor length, material density, lump size, moisture, dust control, loading method and structural corrosion protection |
| Cleated Incline Belt Conveyor | 300–1,200 mm | 5–500 t/h | 0.3–2.5 m/s | Approximately 15–30°, depending on cleat design and material characteristics | Bagged goods, cartons, packaged food, agricultural products and inclined feeding lines | Modular cleats, tool-free belt replacement, servo-compatible control and hygienic conveyor frames | Cleat height and pitch, belt material, product stability, sanitation requirements and discharge height |
| Chevron Pattern Belt Conveyor | 400–1,800 mm | 50–3,000 t/h | 0.8–3.5 m/s | Typically 17–25° for many bulk materials | Coal, sand, gravel, grain, wood chips and recycled materials | Improved grip patterns, lower-noise roller systems and automated belt tracking | Pattern height, material abrasiveness, cleaning method, return-side buildup and maximum incline angle |
| Pipe Belt Conveyor | 200–1,000 mm belt diameter | 100–4,000 t/h | 1.0–5.0 m/s | Routes may include steeper sections than open troughed conveyors, subject to material and design | Dust-sensitive bulk transport, crossing roads, environmentally controlled routes and long-distance conveying | Sealed material transport, reduced spillage, remote diagnostics and route optimization for complex layouts | Pipe diameter, minimum curve radius, belt flexibility, loading and discharge transitions, inspection access and cleaning provisions |
| Overland Belt Conveyor | 800–2,400 mm | 1,000–15,000 t/h | 2.5–7.5 m/s | Usually designed with moderate gradients and controlled vertical curves | Long-distance transport of ore, coal, limestone, aggregates and other bulk materials | Regenerative braking, distributed drive systems, digital twins, condition-based maintenance and optimized route energy use | Topography, horizontal curves, dynamic belt tension, starting requirements, emergency stopping, access roads and lifecycle energy cost |
| Mobile Telescopic Belt Conveyor | 500–1,200 mm | 50–1,000 t/h | 0.5–3.0 m/s | Usually 0–12° depending on the loading operation | Truck loading and unloading, stockpiling, warehouses, ports and temporary construction sites | Battery-assisted mobility, remote positioning, automated stockpile management and quick-connect electrical systems | Travel distance, ground conditions, extension length, wheel or crawler configuration, safety interlocks and setup time |
| Reversible Belt Conveyor | 400–1,500 mm | 50–2,000 t/h | 0.5–3.0 m/s | Normally up to 10–12° for stable material flow | Storage bunkers, batching plants, distribution systems and two-direction material handling | Variable-frequency drives, automatic belt centering, programmable flow direction and overload protection | Reversible belt construction, pulley design, braking response, chute configuration and control-system compatibility |
| Magnetic Separator Belt Conveyor | 400–1,800 mm | 10–500 t/h | 0.5–2.5 m/s | Usually horizontal or low-angle installation | Recycling, scrap processing, aggregate separation and removal of ferrous contaminants | Higher separation efficiency, sensor-based sorting integration and automatic magnetic cleaning systems | Magnetic field strength, material burden depth, belt speed, tramp-metal size, cleaning access and electrical safety |
| Food-Grade Sanitary Belt Conveyor | 200–1,200 mm | 1–100 t/h | 0.1–1.5 m/s | Generally 0–20°, depending on product and belt surface | Food processing, beverage packaging, pharmaceuticals and clean manufacturing | Washdown-ready designs, hygienic stainless-steel frames, tool-less disassembly and data-enabled production monitoring | Food-contact belt compliance, cleanability, drainage, weld quality, temperature range, sanitation chemicals and hygienic design |
| Warehouse Package Belt Conveyor | 300–1,000 mm | Up to 3,000 packages/h per line, depending on package size and spacing | 0.3–2.0 m/s | Normally horizontal; inclined sections commonly use cleats or rollers | Parcel handling, e-commerce fulfillment, baggage handling and distribution centers | Warehouse-control integration, barcode and vision interfaces, modular plug-and-play sections and predictive maintenance | Package dimensions, line speed, accumulation method, noise level, controls integration, guarding and emergency-stop layout |
| Heat-Resistant Belt Conveyor | 500–2,000 mm | 100–5,000 t/h | 0.8–4.0 m/s | Usually up to 15° for loose hot materials | Cement clinker, foundry sand, sintered materials, ash and hot aggregates | Improved heat-resistant rubber compounds, thermal monitoring, fire-risk detection and optimized cooling zones | Continuous material temperature, peak temperature, exposure duration, belt cover compound, fire resistance and cooling requirements |
| Underground Mining Belt Conveyor | 800–2,400 mm | 500–10,000 t/h | 2.0–6.0 m/s | Designed according to mine geometry, material properties and safety regulations | Coal, potash, salt, hard-rock mining and underground transfer systems | Real-time belt rip detection, distributed drives, methane-compatible monitoring and automated fire protection | Explosion-risk classification, belt fire resistance, belt tension, take-up arrangement, ventilation, inspection access and local mining standards |
Technical ranges are typical preliminary-selection values. Final specifications should be confirmed through engineering calculations based on material properties, route geometry, duty cycle, applicable safety standards and local operating conditions.
Rob was always very honest and upfront about everything and took the time to explain everything I needed.
“highly recommended. They provided us with a great storage container with ontime services.”
“Bought a used container, its perfect, no leaks and in good condition.”
“Good service and prompt delivery. A great option for temporary storage at a decent price.”
Join our mailing list to get the latest storage container inventory and offers